
 : +86 15874211461

Diamond & CBN Grinding Wheels
SinoGrind manufactures precision diamond grinding wheels and CBN grinding wheels in resin, metal, vitrified, and electroplated bonds.
View ProductSelect the symptom you see, the workpiece and the wheel setup. The wizard ranks likely causes and gives the first checks to make. It covers diamond, CBN and conventional wheels.
Select the symptom you see, the workpiece and the wheel setup. The wizard ranks likely causes and gives the first checks to make. It covers diamond, CBN and conventional wheels.
Check coolant flow and nozzle placement first, then depth of cut and wheel condition. A dull or glazed wheel and a wheel that is too hard are common causes.
Aluminium is soft and ductile; a dense wheel, fine grit, dry cutting or poor lubricant lets the metal weld to the wheel face. Use a coarse open wheel and flood coolant.
Wheel imbalance, runout, poor workholding, machine rigidity, a hard/glazed wheel or a speed/feed resonance. Balance and true the wheel first.
No. Diamond reacts with iron at grinding temperature; use CBN for hardened steel and cast iron.
These tools provide preliminary guidance based on general engineering principles. Every grinding application has unique variables — wheel specification, machine condition, coolant strategy, and process targets. With over 20 years of experience manufacturing diamond and CBN superabrasive wheels, the SinoGrind engineering team can review your application and recommend a wheel tailored to your exact requirements.
Free consultation • Custom wheel specifications • Global shipping

SinoGrind manufactures precision diamond grinding wheels and CBN grinding wheels in resin, metal, vitrified, and electroplated bonds.
View Product
White, brown, and pink aluminum oxide wheels with vitrified and resin bonds. Ideal for steel, cast iron, tool steel, and stainless steel. Grit sizes 16# to 1000#.
View Product
High-performance centerless grinding wheels and regulating wheels for precision cylindrical grinding.
View Product
Precision diamond dressing tools — rollers, pens, and cutters for truing and dressing grinding wheels.
View Product
High-performance CBN and PCBN cutting tools for hardened steel, cast iron, and aerospace alloys.
View Product
Corundum grinding wheels in ceramic, resin, metal, and rubber bonds for steel, cast iron, and ferrous metal grinding.
View Product
Electroplated mounted rods and mandrels for internal and intricate work.
View product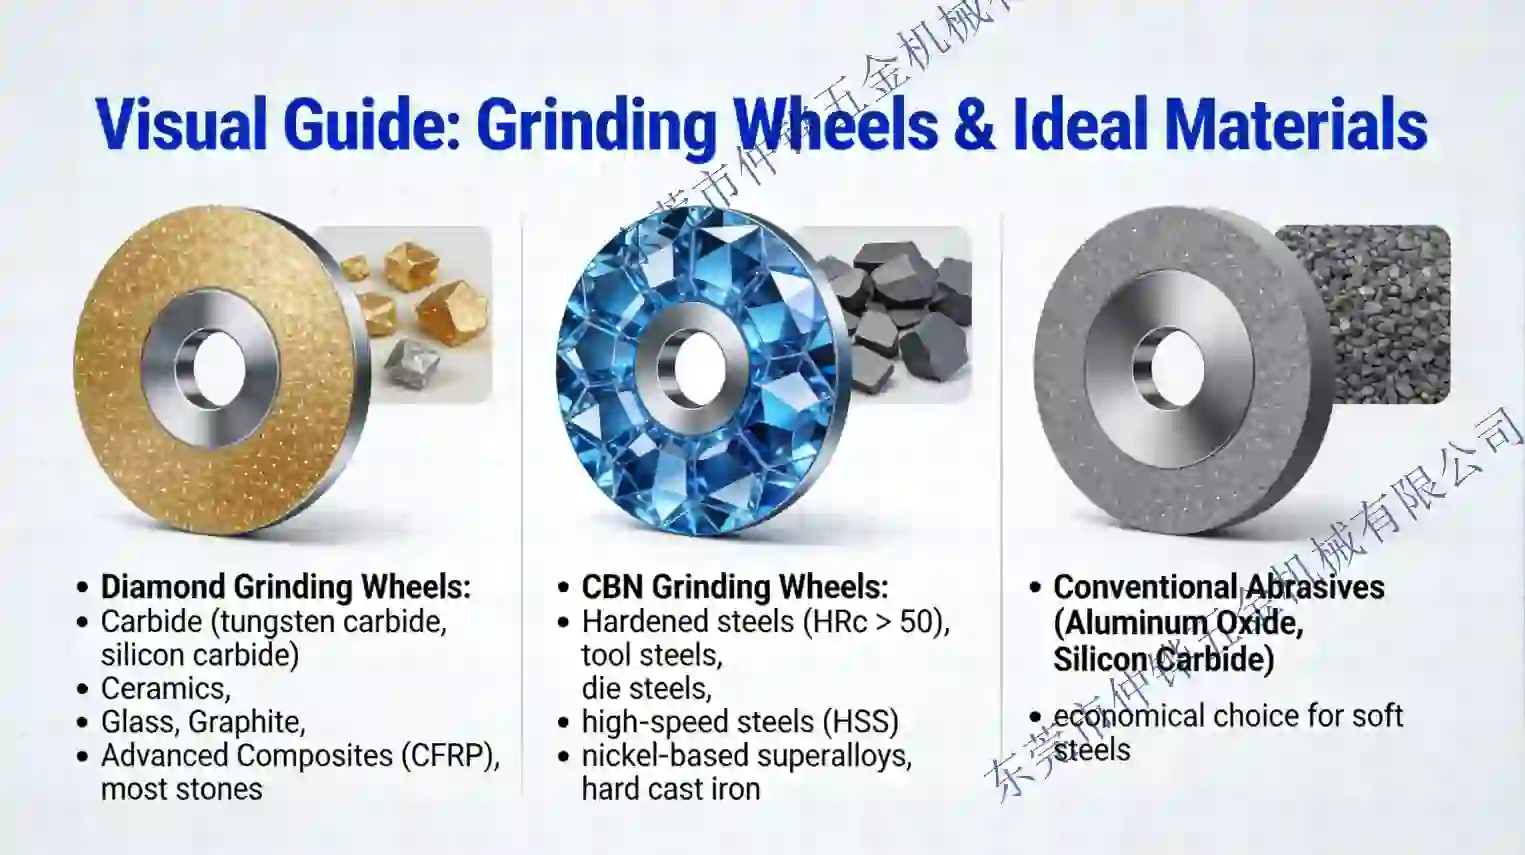
A complete technical guide to selecting the right grinding wheel for your application.
Read More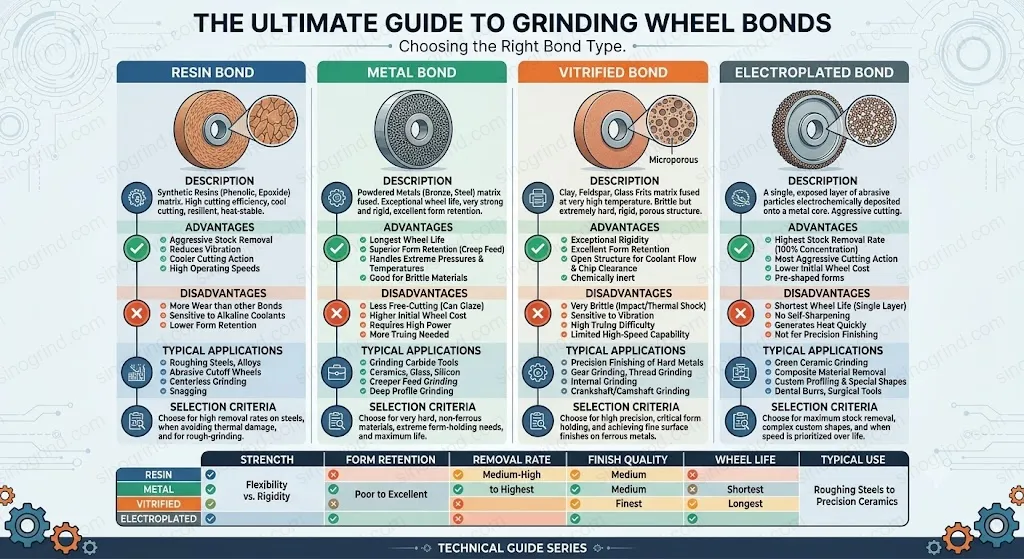
Choosing the right bond type: resin, vitrified, metal, and electroplated.
Read More
Selecting the right grinding wheel for your surface finish requirements.
Read MoreOver 20 years of grinding expertise. Diamond, CBN, and conventional abrasive solutions for precision manufacturing worldwide.




